 +86 139 1520 0887
 info@migreatmachinery.com
The ribbon blender working principle is two spirals on one shaft. A motor and reducer turn the shaft inside a horizontal U shaped trough. The ribbons move the powder in two directions, so the batch circulates and cross-mixes until it is even, and a butterfly valve at the bottom releases it.
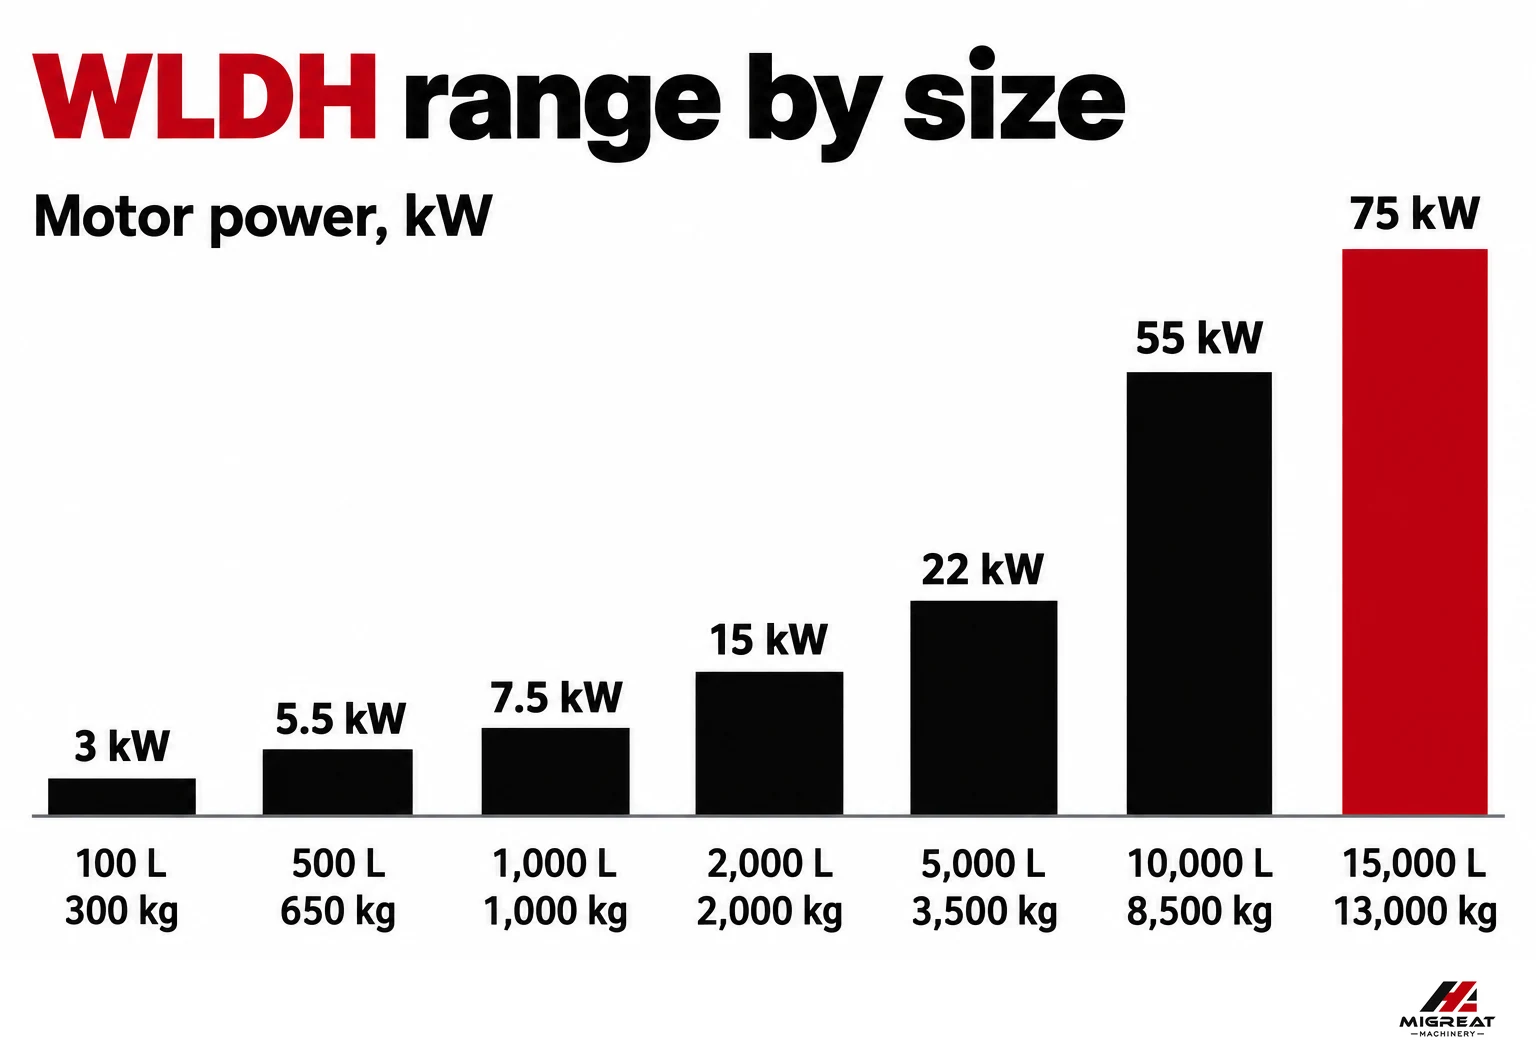
Capacity is chosen as working volume, not machine size. The WLDH range runs from 100 to 15,000 L in 13 models with 3 to 75 kW, and the load coefficient is 0.4 to 0.8, so a 1,000 L trough holds a working batch of 400 to 800 L. The page rates it for powder with powder, powder with liquid, and paste or thick material.
- Main parts are the motor, reducer, cover, trough, feed port, shaft, ribbons, shaft seal and discharge valve
- High homogeneity with little damage to fragile material
- Contact parts in SUS304, 316L, carbon steel or manganese steel
- Discharge by manual or pneumatic butterfly valve
Explanations of the ribbon blender working principle usually show a picture of two spirals and say that they move material in opposite directions. That is true, and it does not tell a buyer how full to run the trough, how long a batch takes or what the blender cannot do. Those three answers are where the money is.
This page explains the ribbon blender working principle in plain terms, names the parts, reads the full WLDH model table, shows how the load coefficient turns into a working batch and works through a sizing example. It also lists the real disadvantages, because every machine has them. It does not cover plough or paddle mixers, which the ribbon, paddle and plough comparison handles.
The ribbon blender working principle in one pass
A ribbon blender works in three moves. Material goes in through the feed port into the U shaped trough, the ribbons on the main shaft move it in two directions until the batch is even, and a butterfly valve at the bottom of the trough releases the batch. Everything else on the machine supports one of those moves.
Load
Material enters through the feed port into the trough. Loading by hand, by vacuum loader or from a hopper all work, and the cover is closed before the batch starts.
Mix
A motor and reducer turn the main shaft. The spiral ribbons on the shaft move the material in two directions, and the batch circulates and cross-mixes until it is even.
Discharge
A manual or pneumatic butterfly valve opens at the bottom and releases the batch. The pneumatic valve suits a line where the operator cannot stand beside the machine.
The ribbon mixer working principle and the ribbon blender principle are the same thing under two names. The word that matters is two directions. A single spiral would push everything toward one end and pile it up there. The second ribbon, wound the other way, carries material back, and the result is a continuous loop along the trough with a gentle tumble across it. Every particle passes through every part of the trough many times in a batch.
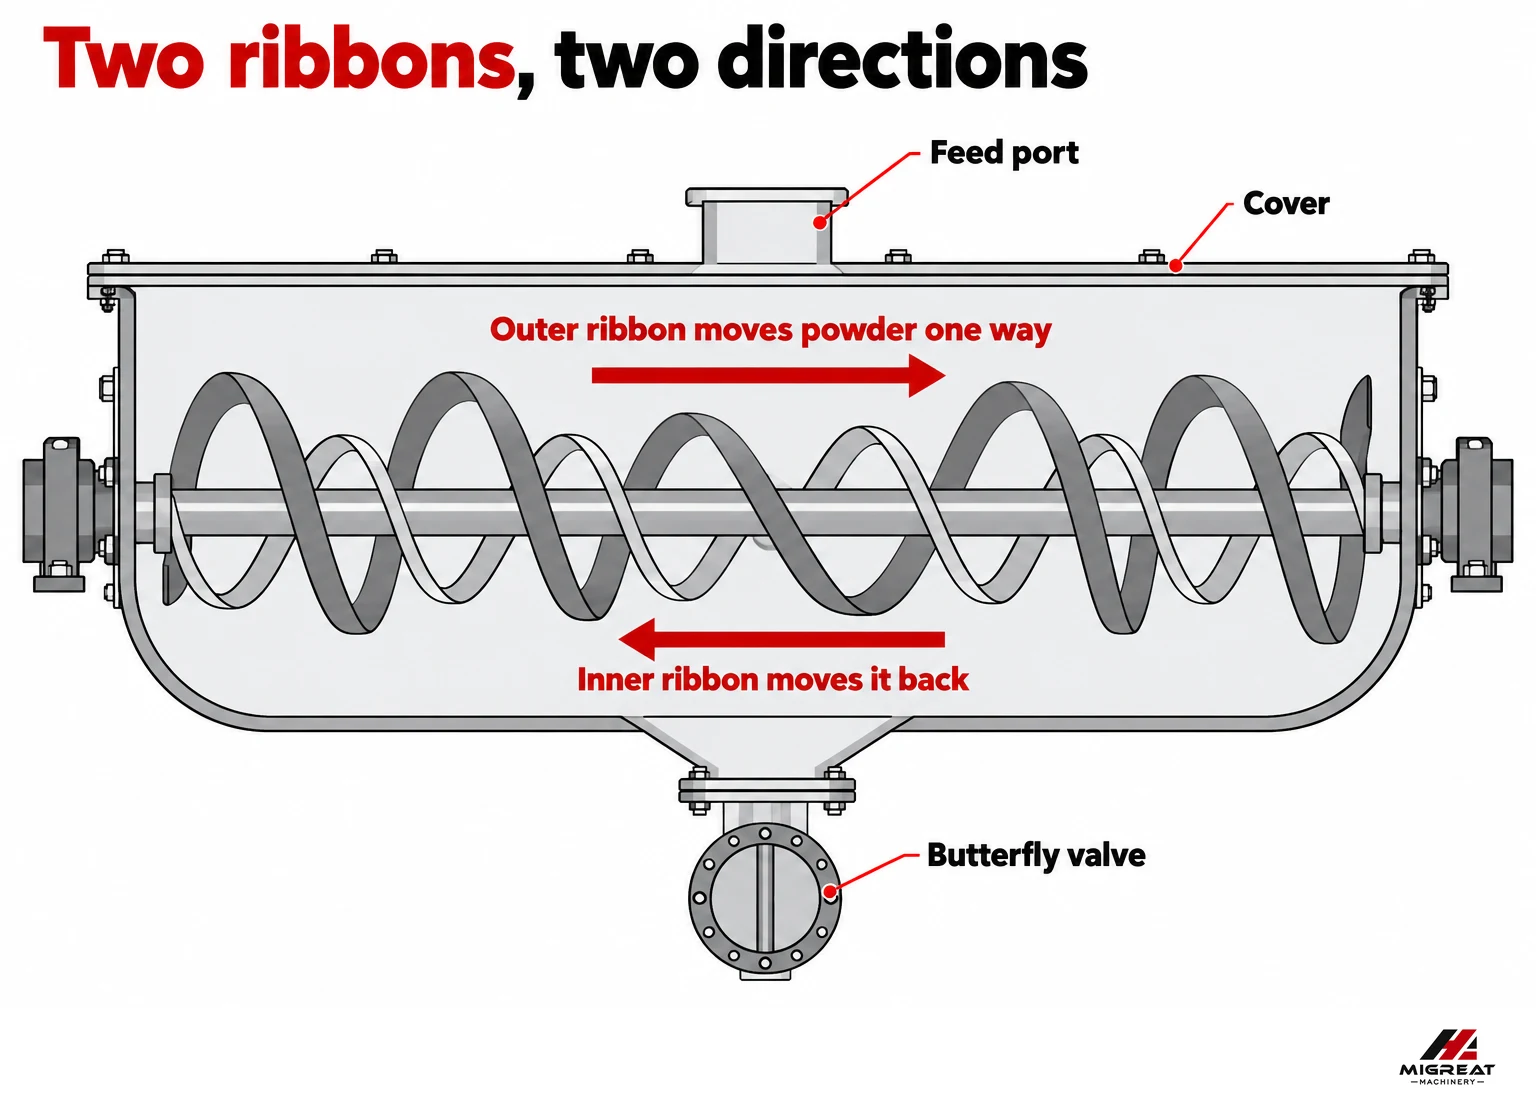
Ribbon blender diagram and parts
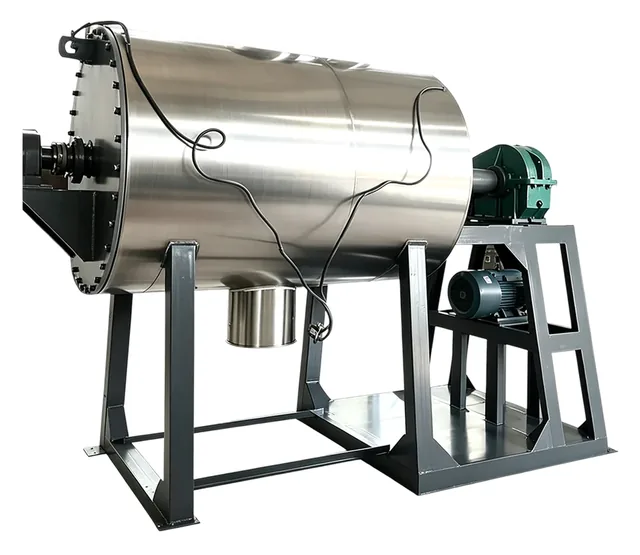
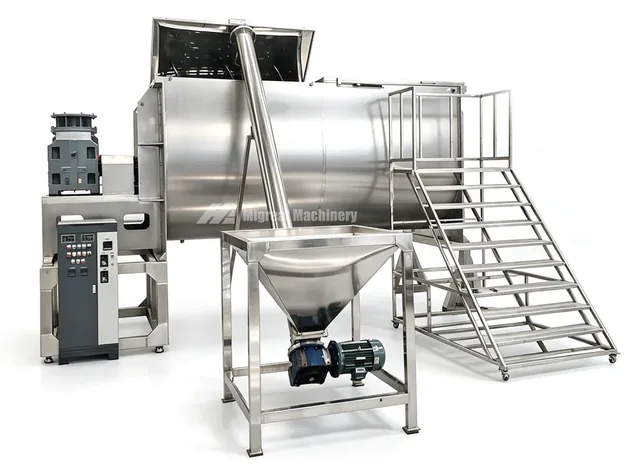
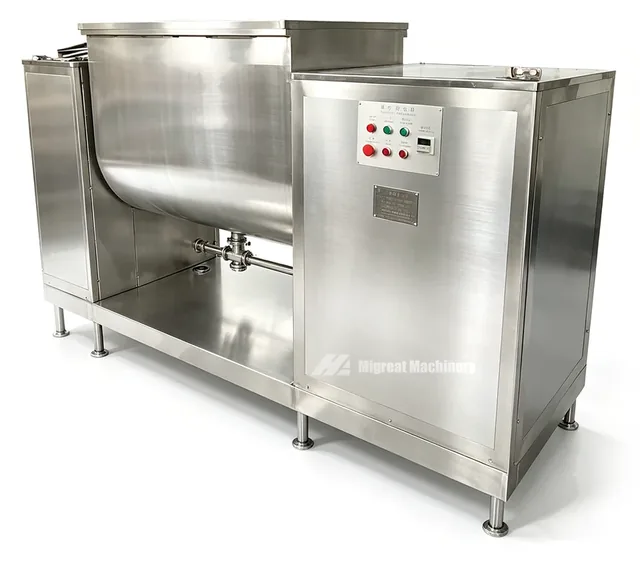
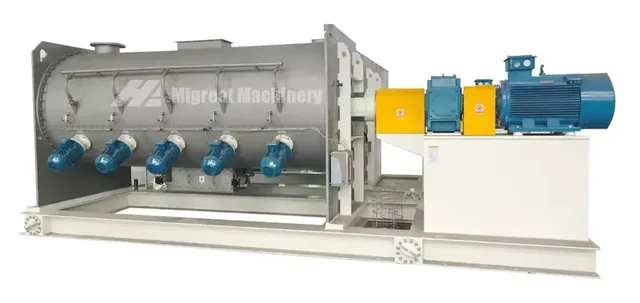
A ribbon blender diagram shows nine parts. The motor, the reducer, the cover, the trough, the feed port, the main shaft, the ribbons, the shaft seal and the discharge valve. A platform and a control cabinet complete most installations. The photographs show the blender from the side and the ribbons in the open trough.
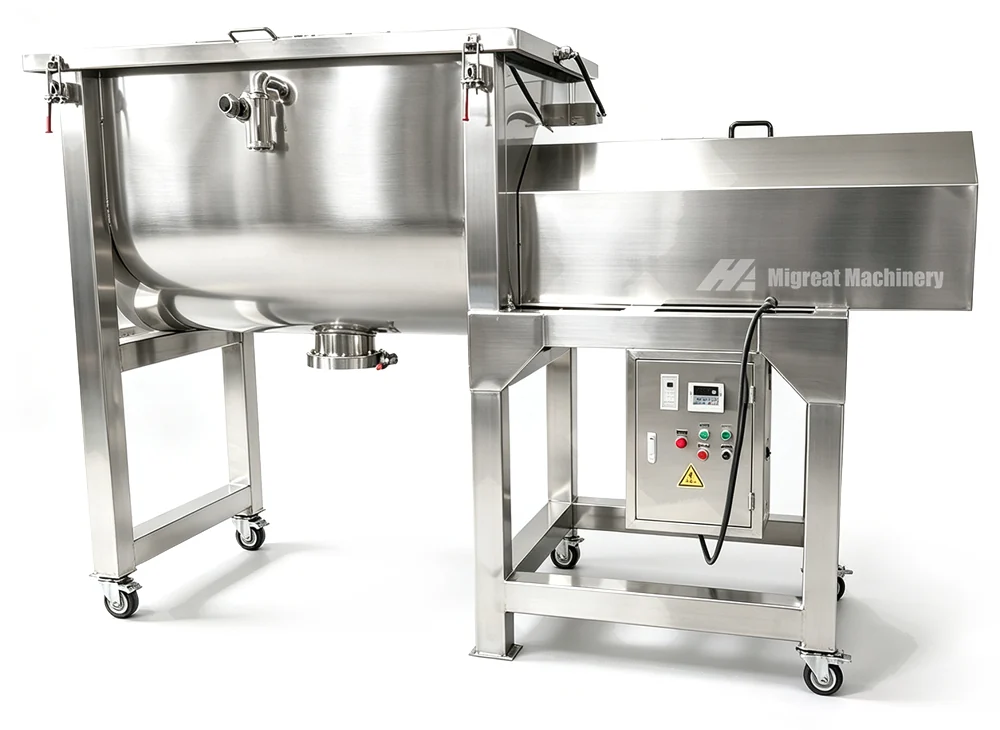
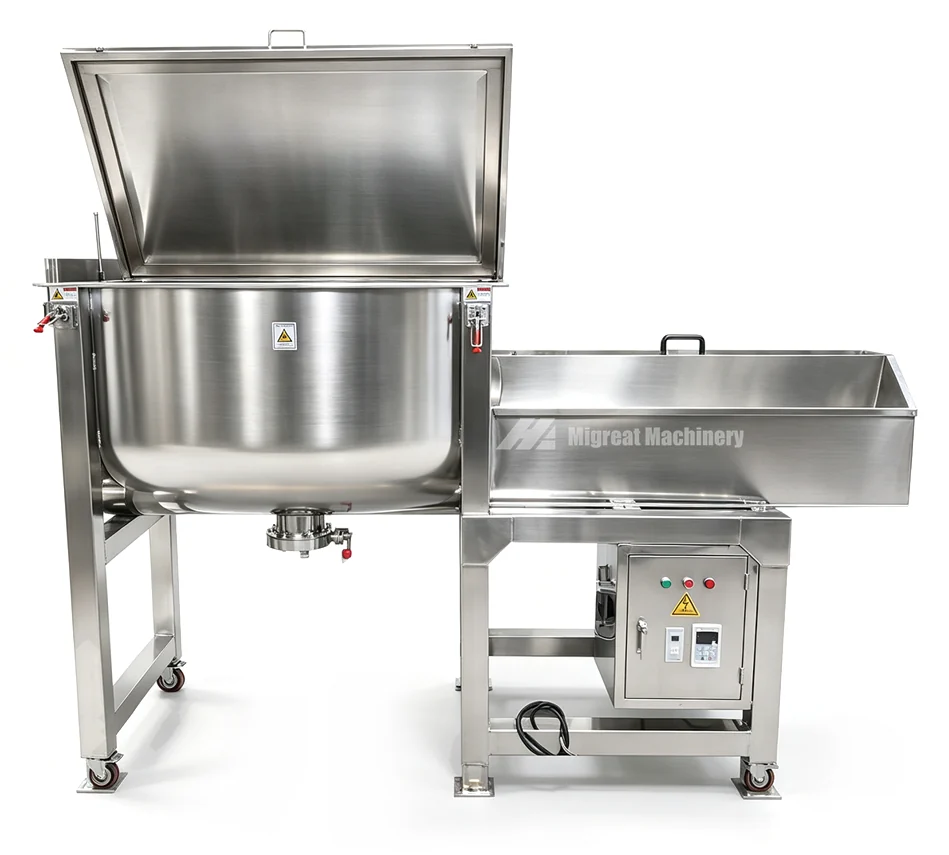
How the two ribbons move the powder
The outer ribbon is wound one way and the inner ribbon the other, on the same shaft. As the shaft turns, the outer ribbon pushes material along the trough in one direction and the inner ribbon pushes it back the other way. The trough is a closed loop for the powder, and the mix comes from the shear between layers moving in opposite directions.
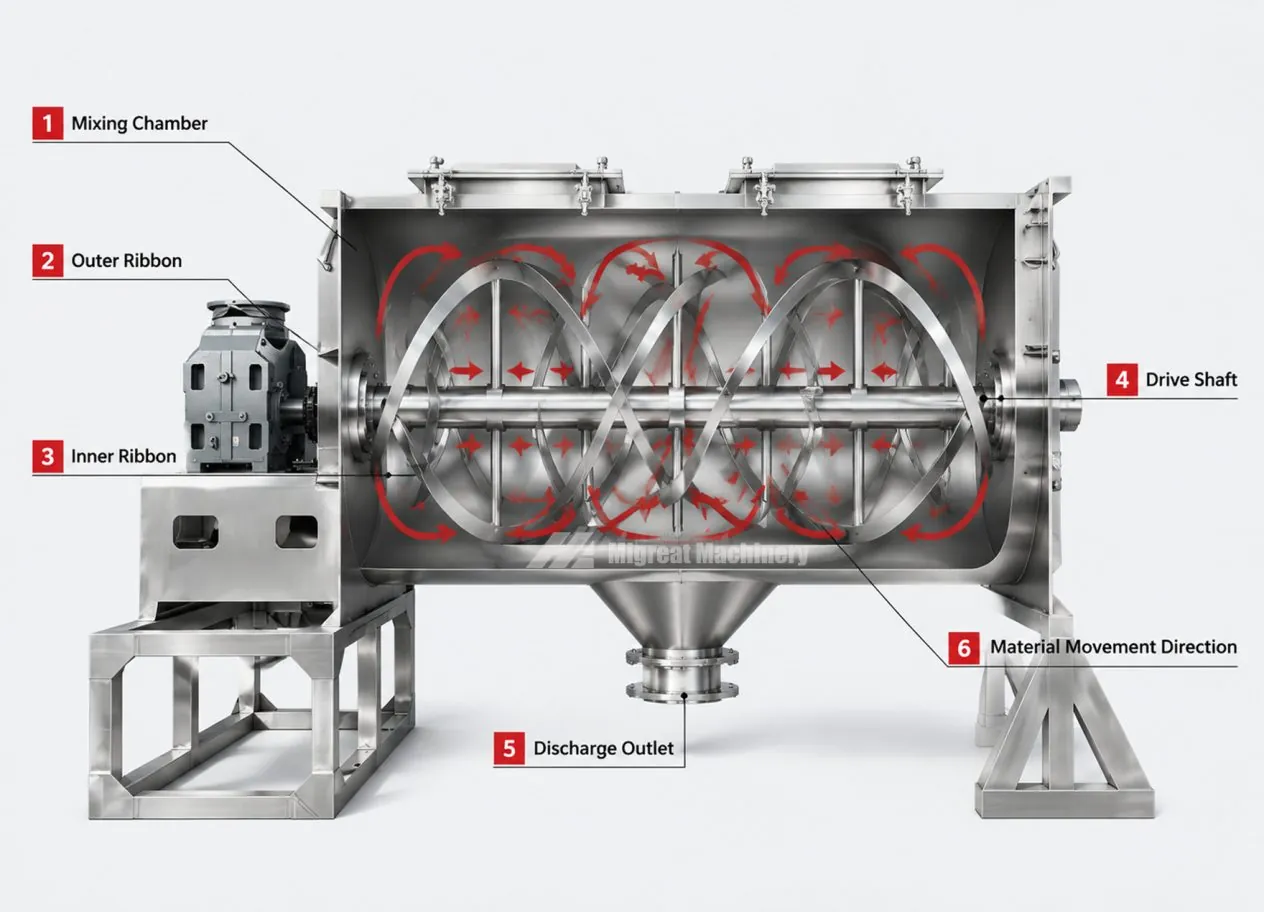
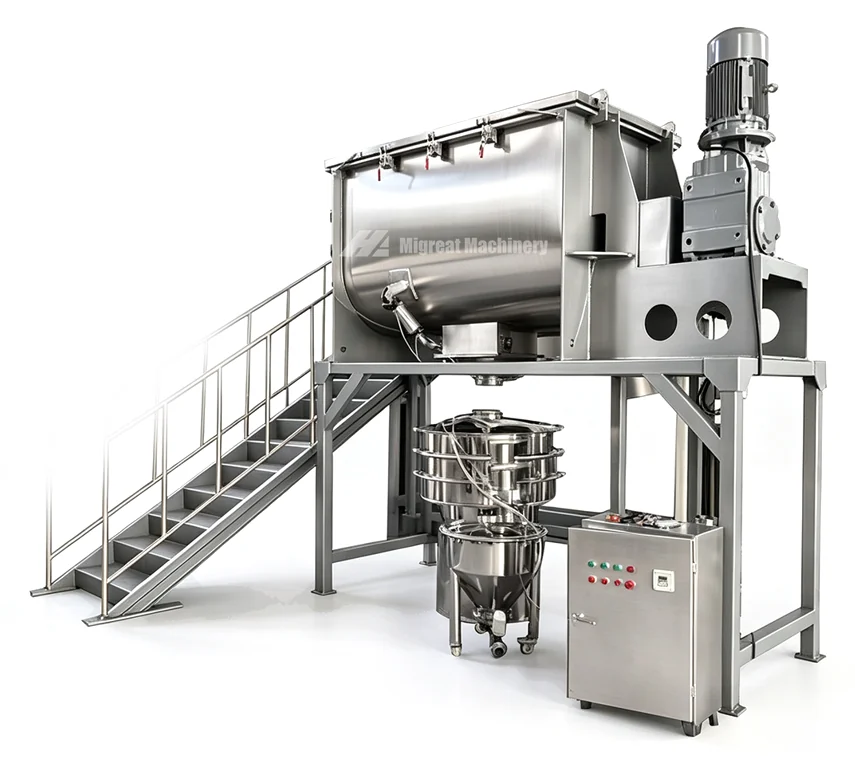
That action explains the strengths and limits. It mixes fast because the powder is forced through itself, and it handles large batches because the shaft and ribbons reach the whole trough. The page states high homogeneity with little damage to fragile material, which is what you would expect from a large mass that is turned and not struck. The same action cannot mix a very small batch well, because the ribbons need enough powder around them to circulate it.
Mixing time and how to test uniformity
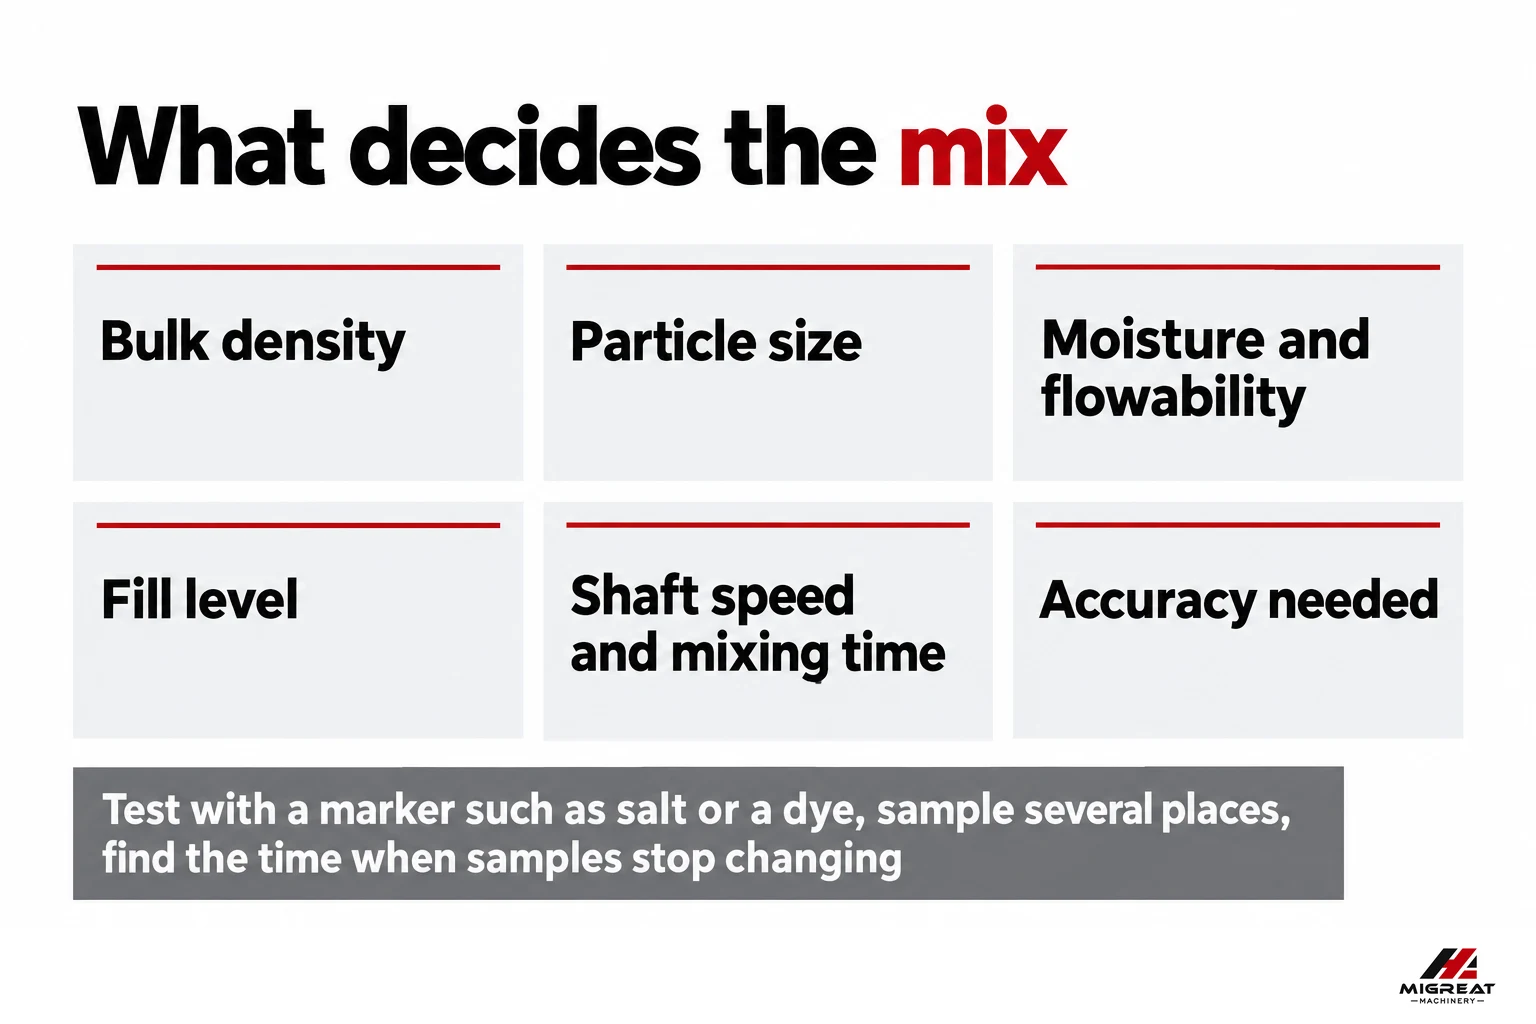
The WLDH page gives no mixing time, and that is a straight answer. The time depends on the recipe, the fill level and the shaft speed, and it can only be found by testing. Run the blender with a marker such as salt or a dye in the recipe, take samples from several places at set times, and compare them. The time at which the samples stop changing is the minimum mixing time for that recipe.
Running longer than that does not help. In a ribbon blender it wastes energy, and with powders that differ in density or size it can start to un-mix them. Write the sampling points, the marker and the allowed spread into the specification so that both sides test the same thing. The factors that matter are the bulk density, particle size, moisture and flowability of the powder, the fill level, the shaft speed, the mixing time and the accuracy you need.
Ribbon blender capacity and the load coefficient
The size of a ribbon blender is its total volume, and the batch it can mix is a fraction of it. The page states a load coefficient of 0.4 to 0.8. A 1,000 L blender therefore mixes a working batch of 400 to 800 L. Where in that range to run depends on the powder. A free flowing powder can be run near 0.8, and a light, fluffy powder is run lower so that the ribbons can move it.
The full range has 13 models, and the table shows nine of them. The sizes in between are WLDH-1500, 4000, 6000 and 8000. Power rises more slowly than volume, from 3 kW for 100 L to 75 kW for 15,000 L, which is one reason the big blenders are economical per liter. The page says sizes are for reference and can be changed to suit your plant.
A worked sizing example
A plant mixes a seasoning at 2,000 kg per batch and four batches a shift. The powder has a bulk density of 0.6 kg per liter, so one batch is about 3,300 L of powder. At a load coefficient of 0.7 the trough must be about 4,800 L in total, which points to the WLDH-5000 at 22 kW. At 0.5 it would need 6,600 L, which is more than the WLDH-6000 holds and points to the WLDH-8000.
The choice between those depends on how the powder flows and on the mixing time found in the trial. If the trial shows the batch is even at a fill of 0.7, the WLDH-5000 is enough. If the powder is light and needs a lower fill, the next size up is safer. Do not choose the largest size to be safe, because a ribbon blender run at a low fill mixes badly and wastes power.
Adding liquid, and mixing paste
The page rates the WLDH for powder with powder, powder with liquid, and paste or thick material. Liquid is usually added through a spray line over the powder while the ribbons turn, so that it spreads before it forms lumps. The page for the WLDH does not list a spray system or choppers as options. Ask your supplier whether they can be fitted for your recipe.
When the recipe is mostly liquid or the feed forms lumps, a plough mixer with choppers is built for the job, and the comparison page explains the difference. Adding a small amount of oil or water to a dry blend is a different matter, and a ribbon blender handles it well if the liquid is added slowly and the batch is mixed long enough for it to disperse.
Discharge, residue and cleaning
The butterfly valve at the bottom of the trough releases the batch, and it can be manual or pneumatic. A little powder is left in the valve seat and around the shaft ends, and the amount depends on the powder. For allergen or color changeovers the residue is the most important number in the quotation. Ask how much stays, and how the machine is washed or purged between products.
Cleaning a trough with a shaft and ribbons takes more time than cleaning a round or conical vessel, because the ribbons are in the way. The page says the ribbons are stainless steel and easy to clean, and an open cover helps. A platform gives access to the feed port. Plan the washdown, the drains and the drying step as part of the machine.
Contact materials and hygiene
The WLDH is offered in carbon steel, manganese steel, SUS304 or 316L, or a combination. Food, pharmaceutical and supplement powders usually need stainless steel on every contact surface. Abrasive material such as some minerals and building powders may call for manganese steel, which wears more slowly. Say what the powder is when you ask, because the material choice changes both the price and the life of the ribbons.
The page lists the applications as milk, coffee and protein powder, spice, flavor and seasoning, supplement powder and additives, and putty powder, gypsum, pigment and dyes. That is a wide spread, and it is the reason the contact material is a quotation item and not a fixed spec.
Advantages and disadvantages of a ribbon blender
The advantages are plain. It handles large batches, it mixes with high homogeneity, it can take liquid and paste, it is simple to run and maintain, and it comes in a very wide size range. The page also lists easy operation, low noise on the motor and movable wheels.
The disadvantages of ribbon blender use are as plain. It is a poor choice for very small batches, it leaves some residue in the valve and at the shaft ends, it is slower to clean than a tumble blender, and its action is stronger than a tumble blender, so very fragile material needs a test. It can also struggle with powders that differ greatly in density, because the ribbons move material but do not stop it separating on discharge. The V blender against ribbon blender page compares those points with the tumble machines.
Loading and discharging in a line
A ribbon blender rarely stands alone. Material arrives from a hopper, a silo or a vacuum loader, and the batch leaves through the valve to a packer or a holding bin. The video of the 2,000 L machine shows the usual large plant arrangement, a horizontal ribbon mixer fed by a screw conveyor from a silo three times its volume. The silo holds the ingredients, the conveyor meters them, and the blender mixes them in batches.
The loading step decides the dust, and the discharge step decides the residue and the cleaning time. A vacuum loader keeps dust out of the room during loading, and a pneumatic discharge valve lets a controller run the cycle without an operator at the machine. Plan the heights, because the trough sits on a platform and the discharge valve needs room beneath it for a bin or a conveyor.
Scaling from a trial to production
A trial on a small blender predicts a large one only if the recipe and the fill level are the same. The mixing time does not scale with volume in a simple way, because the ribbon tip speed and the path length change with the size of the trough. A common approach is to run the trial batch at the planned fill, measure the sample spread against time, and then ask the supplier for the time they expect in the full size machine. Confirm it again at commissioning with samples from the real batch.
Document the result. The recipe order, the loading sequence, the fill level, the shaft speed and the mixing time are the five settings that give the same batch every day. Write them into the operating instruction, and treat any change as a new test.
Problems and how to read them
Most complaints about a ribbon blender trace back to a few causes. Each one has a first check that costs nothing.
Upkeep and wear
Three things wear on a ribbon blender. The shaft seal, which keeps powder out of the bearings. The ribbons, which wear fastest on abrasive material. And the discharge valve seat. Ask for the life of each part on your powder and for the price of spares, and keep a spare seal on the shelf.
Check the clearance between the ribbons and the trough wall at each service. As the ribbons wear, the clearance grows and powder collects in the gap, which slows mixing and raises residue. A simple routine of listening for noise, checking the seal and inspecting the valve will catch most problems before they stop the line. Log each service with the date and the hours run, so that wear can be tracked and spare parts ordered before they are needed.
Where the ribbon blender working principle fits
The ribbon blender working principle suits any dry or damp blend that needs a large, even batch. In food plants it blends spice and seasoning, beverage powder, flour and grain powder and nutritional powder. In nutraceutical plants it mixes functional ingredients and supplement powders. In chemical and building material plants it blends putty powder, gypsum, pigment and dyes, and with thick material it can take a paste.
The common feature is volume. A plant that mixes a few hundred kilograms a day can use a tumble blender, but a plant that mixes tons a shift needs a trough that holds the batch in one go. That is where the load coefficient and the model table earn their keep, because the ribbon blender working principle scales to 15,000 L with the same mechanism and the same cleaning routine.
Questions to put in the quotation
- The working volume at your bulk density, and the load coefficient the supplier assumes.
- The mixing time that meets your uniformity limit, measured on your recipe in a trial.
- The contact materials, the finish and the valve type, with the residue left after discharge.
- Options for liquid addition, vacuum loading, a platform and wheels, and what each adds to the price.
- The seal type, the spare parts list and the lead time for ribbons.
Ribbon blenders at work
The videos show a 2,000 L ribbon mixer working with a silo and screw conveyor, and a new ribbon mixer starting up.


Choose the ribbon blender by working volume at your bulk density, and let a trial set the mixing time.
Send the powder, the batch size, the bulk density and the cleaning needs through the contact page, and an engineer can recommend a WLDH model. The WLDH ribbon mixer page lists every model, and the mixing machines page shows the rest of the range.
Ribbon blender FAQ
QWhat is the ribbon blender working principle?
A motor and reducer turn a main shaft inside a horizontal U trough. Inner and outer spiral ribbons on the shaft move the material in two directions, so the batch circulates and cross-mixes until it is even. A butterfly valve at the bottom then releases it.
QWhat does a ribbon blender do?
It mixes powder with powder, powder with liquid, and paste or thick material, with high homogeneity and little damage to fragile material. The WLDH page lists milk, coffee and protein powder, spice and seasoning, supplement powder, putty powder, gypsum, pigment and dyes.
QHow do I work out the batch size of a ribbon blender?
Multiply the total volume by the load coefficient, which is 0.4 to 0.8 on the WLDH page. A 1,000 L trough therefore mixes 400 to 800 L. Convert to weight with your bulk density, and run lower for light or fluffy powder.
QWhat are the disadvantages of a ribbon blender?
It is a poor choice for very small batches, it leaves some powder in the valve and at the shaft ends, it takes longer to clean than a tumble blender, and its action is stronger on fragile particles. Powders of very different density can also separate on discharge.
QWhat is another name for a ribbon blender?
It is also called a ribbon mixer, a powder blender or a horizontal double ribbon mixer. The page for the WLDH calls it a ribbon blender machine. Some suppliers say paddle mixer for a different design, so check the agitator type in the quotation.
QHow long does a ribbon blender take to mix a batch?
The WLDH page gives no mixing time, because it depends on the recipe, the fill level and the shaft speed. Find it by sampling several places in a trial batch at set times. The time at which the samples stop changing is the minimum mixing time.
QCan a ribbon blender add liquid?
The page rates the WLDH for powder with liquid and for paste or thick material. Liquid is usually sprayed in while the ribbons turn, and the page does not list a spray system, so ask whether one can be fitted. A plough mixer with choppers suits recipes that are mostly liquid.